
Building a Waterproof Bag Quality Control System
A waterproof bag quality control system is four inspection gates placed where a fault can still be corrected cheaply: incoming material before a roll is cut, in-process audit at the welding and sewing stations, finished-unit testing before packing, and a packing audit before a carton is sealed. Each gate has an owner, a sample rule and a record, and the fourth is the one most programmes omit. QUANZHOU JUNYUAN BAGS runs lot acceptance at AQL 2.5 under ISO 2859-1, but sampling only protects the shipment, and the three gates before it stop a fault reaching the sample. This page sets out what happens at each gate, how a fault is ranked, what the corrective action loop looks like, and how to write the system into a purchase order.
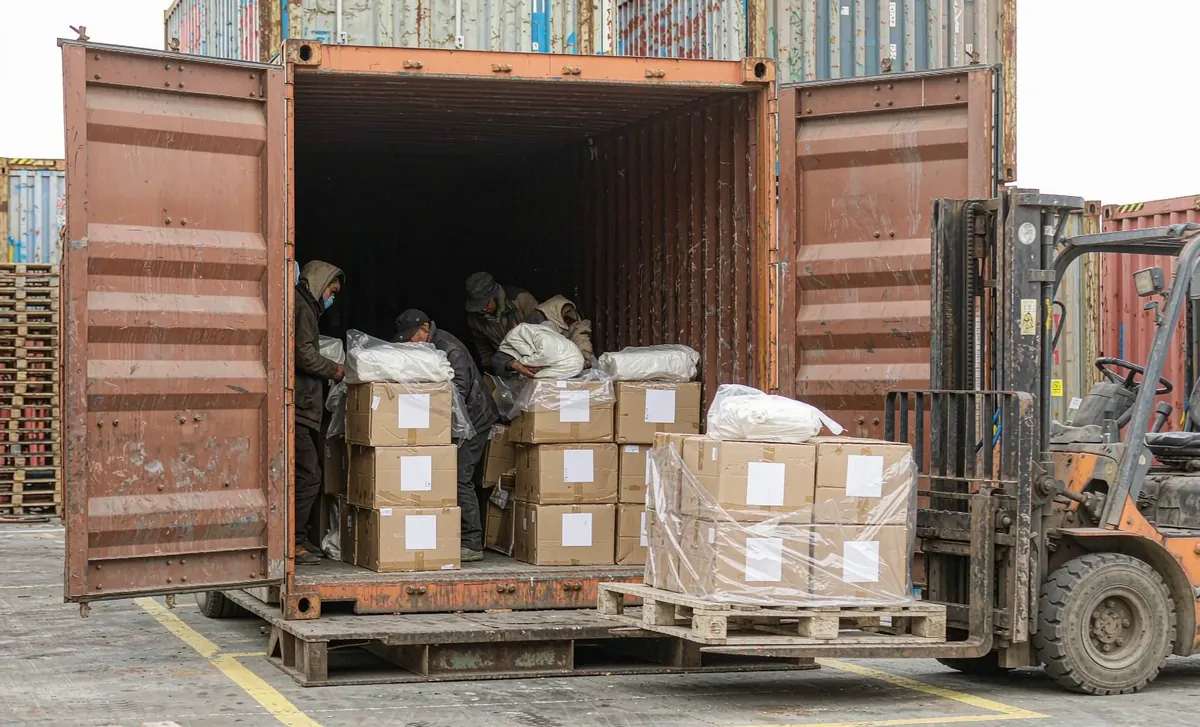
Table of Contents
- Four Inspection Gates and Who Signs Each One
- Incoming Material Checks Before a Roll Is Cut
- In-Process Audit at the Welding Station
- Sewing Defects Catalogued by Root Cause
- Tape Bond Checked at the Start, Middle and End of a Seam
- Water Ingress Tests on Finished Units by Lot
- How a Bench Inspector Ranks a Fault in Under a Minute
- The Packing Bench Audit Before a Carton Is Sealed
- Corrective Action Loop From a Failed Lot
- Records That Make a QC System Auditable
- QC Cost as a Share of a 500-Piece Order
- QC Requirements Written Into the Purchase Order
- What to Record When You Cannot Attend the Inspection
- Frequently Asked Questions
- People Also Ask
Four Inspection Gates and Who Signs Each One
A quality control system for waterproof bags is not a single inspection at the end. It is a sequence of gates placed at the points where a fault is still cheap to correct, and the cost of a fault rises by roughly an order of magnitude at each gate it passes. A coating fault found on a roll costs a roll. The same fault found in a finished body costs the body. Found in a packed carton it costs the carton, and found by a customer it costs the relationship.
The four gates are incoming material, in-process, finished-unit and packing. Each has a different owner, a different sample rule and a different record. Incoming is owned by the material store, in-process by the line supervisor, finished-unit by the quality team, and packing by the packing supervisor with a quality counter-check.
The gate most programmes omit is the fourth. A shipment can pass finished-unit testing and still arrive with the wrong carton count, a mismatched colourway split, missing hangtags or a marking error, and every one of those generates a claim that has nothing to do with the product. Packing is where a correct product becomes a wrong shipment.
- Incoming: owned by the material store, sample by roll, record against the roll number.
- In-process: owned by the line supervisor, sample by station and by hour, record against the shift.
- Finished unit: owned by the quality team, sample by lot under ISO 2859-1, record against the lot number.
- Packing: owned by the packing supervisor with a quality counter-check, sample by carton, record against the carton mark.
- A fault found at a later gate costs roughly ten times what it cost at the earlier one.
Incoming Material Checks Before a Roll Is Cut
Everything downstream depends on what arrives, and incoming is the only gate where a rejection costs almost nothing. The checks are few and quick: confirm the roll against the purchase specification, check shade against the approved reference under defined lighting, check gauge or weight against the tolerance, and test head on specimens taken from more than one point.
The multi-point head test is the one that catches process instability at the mill. A single specimen from the outer end of a roll can measure well on a roll that has pinholes further in, because a coating line that skinned over early produces damage in patches rather than uniformly. Three specimens across the width, or across the length on a long roll, cost a few minutes.
Shade is the second one that matters commercially. Colour is approved against a reference swatch under a defined light source, and the approval has to happen before cutting rather than after assembly, because a shade difference discovered on a finished body is a finished-body problem while the same difference discovered on a roll is a phone call to the mill.
- Confirm the roll against the specification: construction, coating type, gauge or weight, and colour reference.
- Check shade against the approved swatch under a defined light source, not under warehouse lighting.
- Test head at three points rather than one, and record all three results.
- Check for blocking, creasing or surface contamination before the roll is mounted.
- Assign a roll number and carry it through to the cut work order and the finished lot record.
In-Process Audit at the Welding Station
Welding is the process that decides waterproofing on most bags in this category, and it is also the process most sensitive to drift. Radio-frequency and hot-air parameters move with electrode condition, with material temperature, with ambient humidity and with operator technique, which means a station that was set correctly at the start of a shift can be producing marginal seams by the end of it.
The audit is therefore run by time as well as by count. A supervisor takes a seam from the station at defined intervals and peel-tests it, recording force and failure mode. The failure mode is the diagnostic part: adhesive failure at the interface points to a material or primer problem, cohesive failure within the film points to a parameter problem, and a burnt or thinned seam points to excess energy.
The value of the record is in the trend rather than in the individual result. A peel force that is drifting downward across a shift, even while every individual result still passes, is a station that will fail before the shift ends, and catching the trend costs one intervention rather than one re-run.
| Observation at the bench | What it usually indicates | Corrective direction |
|---|---|---|
| Adhesive failure at the interface | Material, primer or surface contamination | Check the roll, the primer and the surface before touching parameters |
| Cohesive failure within the film | Energy too low or dwell too short | Raise energy or dwell within the established window |
| Burnt, thinned or discoloured seam | Energy too high or dwell too long | Reduce energy, and check electrode condition |
| Result varies across the seam length | Uneven pressure or electrode wear | Check pressure distribution and electrode surface |
| Peel force drifting down within a shift | Thermal or ambient drift | Re-set parameters at defined intervals and record the re-set |
Sewing Defects Catalogued by Root Cause
On a waterproof bag, sewing is where most visible faults originate and where most of them are cosmetic rather than functional. Sorting them by root cause rather than by appearance is what turns a defect list into something actionable, because the same appearance can have three different causes and therefore three different corrections.
A skipped stitch looks the same whatever caused it, but a worn needle, a wrong needle point for the fabric, and a thread tension that has drifted are three separate problems. A puckered seam can be a feed problem, a tension problem or a pattern allowance problem. A broken thread can be a needle heat problem at speed or a thread that is too fine for the load.
The functional subset is the one that matters most in this category and it is small: stitch holes through a waterproof layer, which create a leak path that then has to be taped or sealed; a needle that has cut rather than parted the yarns, which weakens the seam; and a seam allowance that is too narrow for the tape width specified, which leaves an untaped margin.
- Skipped stitch: worn needle, wrong needle point or drifted tension, three different corrections.
- Puckering: feed, tension or pattern allowance, and only one of them is a machine setting.
- Broken thread: needle heat at speed, or a thread rated below the load.
- Stitch holes through a waterproof layer: a functional defect, not a cosmetic one.
- Seam allowance narrower than the specified tape width: leaves an untaped margin that leaks.
Tape Bond Checked at the Start, Middle and End of a Seam
Seam tape is applied hot, under pressure, over a stitched seam, and the quality of the bond depends on temperature, pressure, speed and the cleanliness of the surface. Those four drift along a seam as well as between seams, which is why checking one point on one seam tells a buyer very little.
The check is run at three positions along the seam: the start, where the tape is fed and alignment is most likely to be off; the middle, where the parameters are steady and the result represents the process; and the end, where the tape is cut and the trailing edge is most likely to lift. Each position is peel-tested and the failure mode recorded.
The defect that matters most in service is edge creep, where the tape lifts at its edge and progressively admits water along the seam. It is visible under modest magnification on a fresh seam and it is invisible to the eye, so a visual-only tape check will pass seams that fail an ingress test later in the same week.
- Peel-test at the start of the seam, where feed alignment is most likely to be off.
- Peel-test at the middle, where the parameters are steady and the result represents the process.
- Peel-test at the end, where the cut edge is most likely to lift.
- Inspect the tape edge under magnification for creep rather than by eye alone.
- Record tape width against the specification, since an undersized tape leaves an untaped margin.
Water Ingress Tests on Finished Units by Lot
Finished-unit ingress testing is the test that answers the question the customer will actually ask, and it is the one that has to be run on units from the lot rather than on the approved sample. A sample proves that a design can hold water. Units from production prove that the line can make it, and only the second is worth shipping on.
The method depends on the intended exposure. A spray or shower exposure to AATCC 22 or AATCC 35 suits a product sold as rain resistant. A jet exposure under IEC 60529 suits a product strapped to a deck or a rack. An immersion hold at a stated depth and duration suits a pouch or a dry bag that may go under. Specifying the wrong one for the product gives a result that is true and useless.
Where the result fails, the location of the water is the diagnosis. Water at the closure points to the fold or the seating. Water at a seam points to the weld or the tape. Water through a panel points to the material. Recording the location turns a failed test into a work order instead of an argument.
| Water appears at | Most likely cause | Where the correction belongs |
|---|---|---|
| The closure fold | Insufficient turns, or a fold that has lost memory | Closure instruction and stiffener specification |
| Along a welded seam | Parameter drift, or contaminated surface | Welding station audit and material handling |
| Along a taped seam | Tape edge creep, or width under specification | Tape application parameters and incoming tape check |
| Through a panel | Material fault, pinholing or coating thin | Incoming roll test at multiple points |
| At a hardware fitting | Reinforcement or bonding at the fitting | Fitting sequence and reinforcement design |
How a Bench Inspector Ranks a Fault in Under a Minute
Ranking is the decision that determines whether a shipment goes, and it has to be fast because an inspector may look at hundreds of units. The ranking used is critical, major and minor, and the definitions have to be written down before the inspection rather than negotiated during it.
A critical fault is one that makes the product unsafe or unsaleable, such as a hardware failure under load, a sharp edge, or a missing safety marking. A major fault is one that a customer would return, such as a leaking seam, a torn panel, a closure that will not engage, or a print that is illegible. A minor fault is one a customer would notice and accept, such as a small mark, a slight shade variation within tolerance, or a thread end.
The definitions belong in the purchase order, because the same fault can be ranked differently by two parties and the difference decides whether a lot is accepted. An ingress failure is unambiguously major in this category, and the tolerance for minor faults on a waterproof product is generally tighter than on a dry one because the customer is buying a performance claim.
- Critical: unsafe or unsaleable, including hardware failure under load or a missing safety marking.
- Major: a customer would return it, including a leaking seam or a closure that will not engage.
- Minor: a customer would notice and accept, including a small mark or a thread end.
- Write the definitions into the purchase order before inspection rather than during it.
- On a waterproof product, an ingress failure is always major.
The Packing Bench Audit Before a Carton Is Sealed
Packing is the last opportunity to correct, and the faults found there are administrative rather than technical. The audit is short and it is worth running on every carton: confirm the count, confirm the colourway and size split against the order, confirm the polybag and any desiccant, confirm the hangtag and its barcode against the artwork release, and confirm the carton marking against the shipping instruction.
The count is the one that generates the most claims, because a short carton is discovered at the destination where it is expensive to resolve and easy to dispute. Counting at the bench, recording the count against the carton mark and having the supervisor sign it removes almost all of that exposure.
The second one is the split. An order of 500 pieces per style per colour is frequently shipped as a mixed carton plan, and a carton packed with the wrong proportion of colourways is correct in total and wrong at the destination. Auditing the split carton by carton is the only way to catch it before the container is loaded.
- Count the units and record the count against the carton mark, signed by the supervisor.
- Confirm the colourway and size split in the carton against the order, not just the total.
- Confirm the polybag, desiccant and any insert card are present as specified.
- Confirm the hangtag and barcode against the released artwork.
- Confirm the carton marking and the shipping mark against the instruction.
- Photograph a sealed carton from each lot and keep the photograph with the lot record.
Corrective Action Loop From a Failed Lot
A failed lot is not a disaster and it is not an argument, provided the loop that follows it is defined. The loop has five steps: contain, diagnose, correct, verify and prevent. Most programmes do the first two and stop, which is why the same failure returns on the next order.
Containment means isolating the affected units and the affected material, including any rolls from the same lot that have not yet been cut. Diagnosis means tracing the fault to a production step rather than to a person, because a step can be changed and a person cannot. Correction means reworking or remaking the affected units. Verification means re-inspecting the corrected output at the same level as the original. Prevention means changing the control that allowed it, which is usually a missing or an unwritten check at an earlier gate.
The fifth step is the one with commercial value. A corrective action that ends in prevention reduces the cost of every future order, and one that ends in rework only adds the cost of this one. Asking for the preventive change in writing, and not only for the rework, is the single most useful question a buyer can put after a failure.
- Contain: isolate units and uncut material from the same lot.
- Diagnose: trace to a production step, not to a person.
- Correct: rework or remake the affected units.
- Verify: re-inspect the corrected output at the same level as the original.
- Prevent: change the control that allowed it, and ask for that change in writing.
Records That Make a QC System Auditable
A quality control system is only as good as its records, because a record is what allows a fault to be traced backwards after a customer complaint arrives months later. The minimum set for a bag programme is a roll record, a shift record, a lot record, an inspection report and a corrective action record, and each one needs an identifier that links it to the others.
The linkage is the part that is usually missing. A roll number that does not appear on the cut work order cannot be traced to a finished lot. A lot number that does not appear on the carton mark cannot be traced to a shipment. Without the identifiers, a complaint about one batch becomes a complaint about everything, and the response has to be defensive rather than specific.
Retention matters as much as linkage. Reference samples from each lot, kept for the life of the product plus a margin, allow a returned item to be compared against what was approved rather than against a description. That comparison settles disputes quickly and it is the cheapest insurance in the programme.
| Record | Identifier it carries | What it allows you to answer later |
|---|---|---|
| Roll record | Roll number and mill batch | Which material went into which lot |
| Shift and station record | Date, shift, station and hour | Whether a fault clustered in time |
| Lot record | Lot number linked to roll numbers | Which material is in the complained-about units |
| Inspection report | Lot number, sample size, defect count by class | Whether the lot passed and on what basis |
| Corrective action record | Lot number, root cause step, preventive change | Whether the same failure can recur |
QC Requirements Written Into the Purchase Order
A quality control system that exists only in conversation is not a system. The requirements that determine whether a shipment is accepted belong on the purchase order, in enough detail that two parties reading it separately reach the same conclusion. That means the standard, the level, the defect definitions and the consequence of a failure.
The consequence clause is the one that gets left out and the one that matters. Stating what happens on a failed inspection, whether rework, partial remake, full remake or a delayed balance payment, converts a negotiation into a procedure. Without it, every failure becomes a discussion at exactly the moment both parties have least room to move.
The second clause worth writing is the hold point. A hold point is the stage at which production stops and waits for a result, and on a waterproof programme the useful one is before bulk cutting begins, once the pre-production sample has passed its ingress test. Stopping before cutting costs days. Stopping after assembly costs the run.
- State the sampling standard and the level: AQL 2.5 under ISO 2859-1, with the general inspection level stated.
- State the defect definitions for critical, major and minor, written for this product.
- State the test methods and their acceptance conditions, including duration and closure configuration.
- State the consequence of a failed inspection: rework, partial remake or full remake.
- State the hold point, and who releases it.
- State the records to be issued and when, and tie the balance payment to their issue.
What to Record When You Cannot Attend the Inspection
Most buyers cannot attend every inspection, and the substitute for attendance is not a longer report but a better-defined one. What is needed is a set of photographs tied to identifiers, the raw defect count by class rather than only a pass or fail statement, and the test conditions alongside every test result.
Photographs should show the carton as opened, the defect with something for scale, and the carton mark with the lot number legible. A photograph of a defect without a scale and a photograph of a carton without its mark are both nearly useless six weeks later, when the question is whether a specific lot is affected.
The raw count matters because a pass or fail statement hides the margin. A lot that passed with one major and a lot that passed with none are very different shipments, and the second of the two tells a buyer something useful about the next order. Asking for the count by class costs nothing and provides a trend.
QUANZHOU JUNYUAN BAGS was established in 2014, with our founder in the bag trade since 2004, and lot acceptance is recorded at AQL 2.5 under ISO 2859-1 with defect classes defined before the inspection opens. Head is reported to ISO 811 across a band from 10,000 mm for lightweight builds to beyond 20,000 mm for heavy-duty ones, ingress is tested to IEC 60529 with the method and duration recorded, and spray and shower behaviour is checked to AATCC 22 and AATCC 35. Capacity at our validated production partner facility is verified by SGS at 4,950 square metres, 7 production lines, 149 pieces of equipment, 137 staff and 200,000 pieces per month, with market documentation able to cover CE, CPC, RoHS and REACH, with QC run to ISO 9001-aligned procedures. Sampling runs 6 to 10 working days, or 12 to 15 for a complex build, and bulk runs 35 to 50 days, quoted FOB Xiamen on T/T 30% deposit and 70% before shipment.
To have a quality protocol written into an order, write to service@junyuanbags.com or message the team on WhatsApp at +86 177 5002 0688. The methods behind each gate are described in the water ingress test methods guide, the spray and shower methods are explained in the AATCC 22 spray test guide and the AATCC 35 rain test guide, and a protocol can be built from the quality page.
Frequently Asked Questions
Q1: How many inspection gates does a waterproof bag programme need?
A: Four, placed where a fault is still cheap to correct: incoming material before a roll is cut, in-process audit at the welding and sewing stations, finished-unit testing before packing, and a packing audit before a carton is sealed. The cost of a fault rises by roughly an order of magnitude at each gate it passes.
Q2: What should be checked on an incoming fabric roll?
A: Confirm the construction, coating type, gauge or weight and colour reference against the specification, check shade against the approved swatch under defined lighting, and test head at three points rather than one. Multi-point testing catches mill process instability that a single specimen from the roll end will miss entirely.
Q3: Why is in-process auditing run by time as well as by count?
A: Because welding parameters drift with electrode condition, material temperature, ambient humidity and operator technique. A station set correctly at the start of a shift can be producing marginal seams by the end of it, and a peel force trending downward within a shift predicts a failure before it happens.
Q4: What does an adhesive failure at a welded seam indicate?
A: It indicates a material, primer or surface contamination problem rather than a parameter problem, so the correction belongs upstream at the roll and the handling. Cohesive failure within the film is the one that points to parameters, specifically to energy too low or dwell too short.
Q5: Why check seam tape at three positions rather than one?
A: Because temperature, pressure, speed and surface cleanliness drift along a seam as well as between seams. The start is where feed alignment is most likely to be off, the middle represents the steady process, and the end is where the cut edge is most likely to lift.
Q6: What is tape edge creep and why does it matter?
A: It is the progressive lifting of a tape edge that admits water along a seam over time. It is invisible to the eye and visible under modest magnification, so a visual-only tape check will pass seams that subsequently fail a water ingress test later in the same week.
Q7: Should ingress testing be run on the approved sample or on production units?
A: On production units. A sample proves that a design can hold water, while units taken from the packed lot prove that the line can make it. Only the second statement is worth shipping on, because tooling, operators and parameters all drift across a production run.
Q8: How is a fault ranked as critical, major or minor?
A: A critical fault makes the product unsafe or unsaleable, a major fault is one a customer would return, and a minor fault is one a customer would notice and accept. The definitions must be written into the purchase order before inspection, and an ingress failure is always major on a waterproof product.
Q9: What is checked at the packing bench before a carton is sealed?
A: The unit count recorded against the carton mark, the colourway and size split against the order rather than the total, the polybag and any insert card, the hangtag and barcode against the released artwork, and the carton marking against the shipping instruction.
Q10: What are the five steps of a corrective action loop?
A: Contain, diagnose, correct, verify and prevent. Most programmes do the first two and stop, which is why failures recur. The fifth step is the one with lasting value, because a change to the control that allowed the fault reduces the cost of every future order.
Q11: What records make a bag quality system auditable?
A: A roll record, a shift and station record, a lot record, an inspection report and a corrective action record, each carrying an identifier that links it to the others. Without linkage, a complaint about one batch becomes a complaint about everything and the response has to be defensive.
Q12: What should a purchase order say about quality control?
A: The sampling standard and level, the defect definitions for critical, major and minor, the test methods with their acceptance conditions, the consequence of a failed inspection, the hold point and who releases it, and which records are issued and when.
Q13: What is a hold point and where should it sit?
A: A hold point is a stage at which production stops and waits for a result. On a waterproof programme the useful one sits before bulk cutting begins, once the pre-production sample has passed its ingress test, because stopping before cutting costs days and stopping after assembly costs the run.
Q14: What should be recorded when a buyer cannot attend the inspection?
A: Photographs of the carton as opened, of each defect with a scale, and of the carton mark with a legible lot number, plus the raw defect count by class rather than only a pass or fail statement. The count reveals the margin, which a pass or fail hides.
People Also Ask
- How do you quality control waterproof bags?
- What is AQL 2.5 for bags?
- How do you test a waterproof seam?
- What is seam tape edge creep?
- What is a critical versus major defect?
- What should a bag QC report include?
- Should I inspect before or after packing?