
Waterproof Bag Seam Sealing: Weld, Tape or Stitch
A waterproof bag almost never leaks through its fabric; it leaks at the join, and the join is where the coating has been melted, pressed or pierced. Six sealing methods are available for a welded shell: radio frequency, hot air, hot wedge, ultrasonic, tape over stitch, and stitch-and-tape hybrids. Each has a different peel strength, a different cycle time and a different failure mode, and the right one depends on the coating chemistry and the geometry of the seam. QUANZHOU JUNYUAN BAGS qualifies the method and the parameter window at 500 pieces per style per colour.
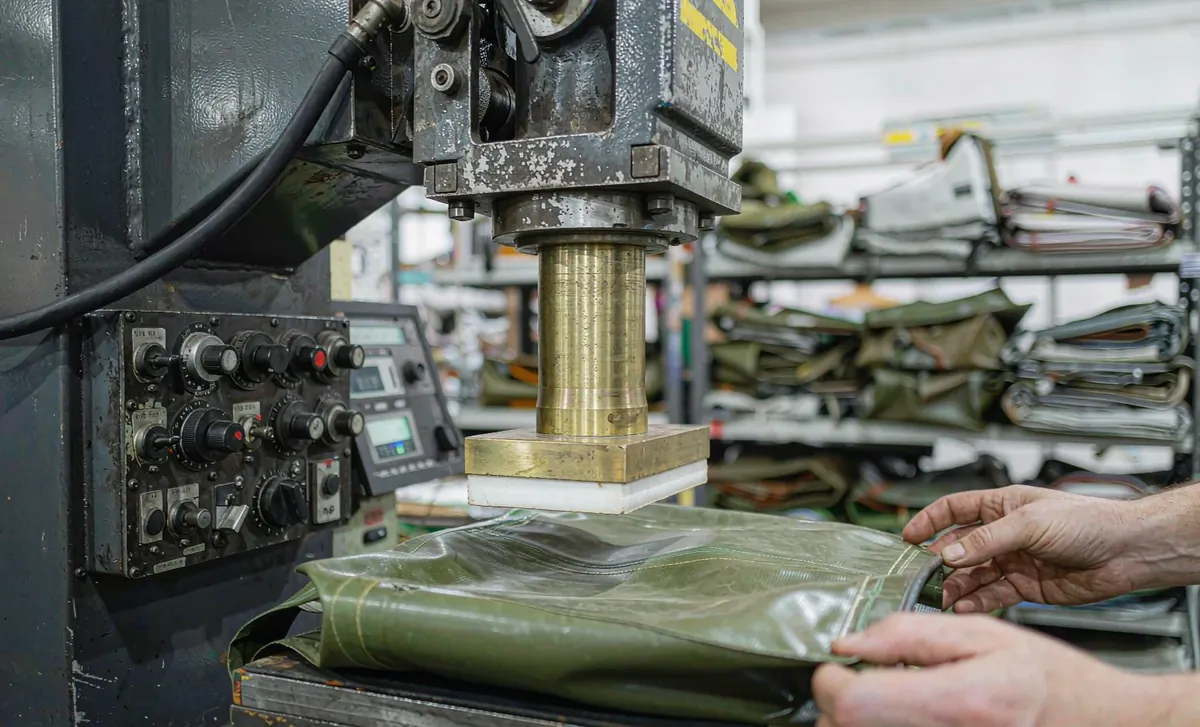
Table of Contents
- Where a Welded Waterproof Bag Actually Leaks
- RF Welding and the Dielectric Heating Window
- Hot Air and Hot Wedge Welding on TPU Shells
- Ultrasonic Welding for Hardware and Light Panels
- Taped Seams Over Stitched Waterproof Construction
- Seam Method Selection Table by Waterproof Bag Format
- Weld Parameter Windows and Where Operators Drift
- Peel Strength Versus Hydrostatic Head at the Seam
- Seam Failure Modes Found in Warranty Returns
- Seam Leak Detection at the Bench and on the Line
- Low-Temperature Seam Flex and Freeze Cycling
- Seam Spec Wording for a Welded Bag Order
- Seam Cycle Time and Cost on a 500-Piece Run
- Frequently Asked Questions
- People Also Ask
Where a Welded Waterproof Bag Actually Leaks
Ask any warranty department where a waterproof bag failed and the answer is almost always the join rather than the panel. The shell fabric carries a coating or a laminate that will hold 10,000 mm on a lightweight style and 20,000 mm and above on a load-bearing one, and it holds that figure across its whole area. The seam is the place where two coated faces have been brought together, where the coating has been melted and re-solidified, and where the barrier is therefore only as good as that operation made it.
Three geometries account for most seam leaks, and they are worth naming because they are predictable and therefore preventable. The first is the multi-ply corner, where three or four layers meet and the electrode cannot press them evenly, leaving a channel at the point where the plies step down. The second is the transition, where a welded seam runs into a stitched or taped section. The third is the termination, where a seam ends in open fabric rather than running off an edge.
The fourth cause is not geometry at all but contamination. A face that carries dust, release agent, finger oil or moisture will not fuse to itself consistently, and the result is a seam that holds in one place and opens in the next. Cleanliness at the weld station is unglamorous and it is the difference between a line that runs at a consistent pass rate and one that produces intermittent failures that no parameter change will fix.
Knowing this changes what a buyer should ask to see. A hydrostatic certificate on the shell tells you the fabric will hold water; it tells you nothing about the join. The evidence that matters is a seam test on the constructed bag: peel values from the actual production method, a leak test on finished units, and a record showing those checks were taken across the run. That is the difference between a supplier who tests a material and one who tests a product.
RF Welding and the Dielectric Heating Window
Radio frequency welding heats the coating from the inside out. The plies sit between two electrodes, a high-frequency field is applied, and the polar molecules in the coating generate heat through dielectric loss while the fabric and the electrode stay comparatively cool. That is why RF is the dominant method on PVC and on many TPU constructions: the heat is generated exactly where the bond has to form, rather than being conducted in from a hot surface.
The window is the set of parameters that produces a good bond: generator output, weld time, dwell under pressure after the generator stops, and electrode force. Too little energy and the coating does not fully melt, giving a seam that peels. Too much and the coating degrades, bubbles or thins to the point where the seam is weaker than the fabric around it. The usable band between those two ends is narrower than most buyers assume, which is why recorded parameters matter.
Material matters as much as setting. PVC responds strongly to a dielectric field and welds readily; TPU varies by formulation and some grades weld poorly on RF while welding beautifully on hot air. Fabric construction, coating thickness and any surface finish all shift the window. This is the reason a shell should never be approved on a data sheet alone, and why we trial-weld every candidate shell at three points across the window before it goes onto a style.
Hot Air and Hot Wedge Welding on TPU Shells
Hot air welding directs a stream of heated air at the interface between two plies and then presses them together under a roller. It heats by convection rather than by dielectric loss, so it is far less sensitive to the chemistry of the coating and it is the default answer where a TPU grade will not respond to RF. It is also the method that tolerates a surface finish better, which matters on shells carrying a fluorine-free repellent.
The trade-off is control and speed. Air temperature, air volume, nozzle distance, roller pressure and line speed all have to hold together, and the operator has more variables to manage than on an RF press. Line speed is generally slower than an RF cycle, and variable speed across a long seam produces variable heat input, so consistency depends on the operator holding a steady hand as much as on the machine holding its setting.
Hot wedge welding is the contact version of the same idea: a heated wedge is drawn between the plies and nip rollers close the seam behind it. It gives more repeatable heat input than a free air stream because the wedge is in contact and at a controlled temperature, and it suits long straight seams on duffels and dry bags extremely well. It is less suited to tight corners and short three-dimensional joins, where the wedge cannot follow the geometry.
Ultrasonic Welding for Hardware and Light Panels
Ultrasonic welding applies high-frequency mechanical vibration through a horn, generating heat by friction at the interface. It is fast, it is localised, and it needs no consumable, which makes it attractive for two specific jobs on a waterproof bag rather than as a general seam method. The first is attaching hardware: a D-ring tab, a strap anchor or a moulded fitting welded to a panel without piercing it.
The second job is closing small features on light panels: a valve port, a small pocket face, a cable pass-through. Ultrasonic handles these cleanly and quickly where an electrode would be disproportionate. What it does not do well is long continuous seams on heavy coated fabric, because the horn can only weld an area roughly its own size at a time, so a long seam becomes a series of overlapping impressions with cold spots between them.
The failure mode to watch for is over-welding at the horn edge. Because the energy is concentrated, too much amplitude or too long a dwell thins the coating locally and can cut through a light shell entirely. On a hardware tab this shows up as a fitting that pulls away with a ring of fabric still attached to it, which looks like a strong bond and is actually a destroyed one.
Taped Seams Over Stitched Waterproof Construction
Stitching pierces the fabric, and every needle hole is a potential leak path, so a stitched waterproof seam is only as good as the tape applied over it. The tape is a thermoplastic film with an adhesive, applied under heat and pressure over the needle line on the inside of the seam. Done properly it produces a seam that is strong in tension and sealed against water, which is why stitched-and-taped construction persists in applications where peel load matters more than ultimate waterproofness.
Tape width is the variable buyers under-specify. A tape has to cover the needle line with margin on both sides, and the margin has to survive the seam being flexed and the bag being packed. Too narrow and the tape edge lifts; too wide and the seam becomes stiff and uncomfortable where it crosses a harness. The window is set by the stitch geometry and by how much the seam is allowed to move in service.
The other variable is the substrate. Tape adheres to the coating, not to the fabric, so a shell with a poor or uneven coating will not hold tape however good the tape is. This is the hidden reason some cheap coated fabrics cannot be made reliably waterproof by any route: they cannot be welded because the coating is inconsistent, and they cannot be taped because the tape has nothing to grip.
Seam Method Selection Table by Waterproof Bag Format
The table below is the shortlisting tool we use when a buyer brings a new format. It is written in the terms that actually decide the choice: what the coating will tolerate, what geometry the seam has to follow, how fast the operation runs, and what the seam has to survive in service. Peel figures are relative bands rather than absolute values because they depend on the shell being used.
| Sealing method | Best suited to | Typical seam peel band | Cycle speed on a long seam | Main limitation |
|---|---|---|---|---|
| Radio frequency welding | PVC and responsive TPU, 3D corners, multi-ply joins | Highest band, approaches parent fabric strength | Fast, one press cycle per seam | Narrow parameter window, sensitive to finish and moisture |
| Hot air welding | TPU grades that resist RF, finished or coated faces | High band, slightly below RF | Moderate, limited by line speed | Operator dependent, more variables to hold steady |
| Hot wedge welding | Long straight seams on duffels and dry bags | High band, very repeatable | Fast on straight runs | Cannot follow tight corners or short 3D joins |
| Ultrasonic welding | Hardware tabs, valve ports, small light-panel features | Good on small areas, localised | Very fast per spot | Not continuous; over-welding thins the coating |
| Tape over stitched seam | Harness attachment, high peel load areas, repairs | Moderate band, governed by tape adhesion | Slow, two operations | Depends entirely on coating quality for adhesion |
| Stitch and tape hybrid | Where a welded seam meets a load-bearing assembly | Moderate band with high tensile strength | Slowest, three operations | Transition point between weld and tape is a leak risk |
Two entries repay a second look. The stitch-and-tape hybrid is where most field failures originate, not because the method is weak but because the transition between a welded run and a taped run is a discontinuity that no single test covers well. Where a design forces that transition, it should be tested as an assembly rather than as two separate seams, because the join between them is the part that fails.
Weld Parameter Windows and Where Operators Drift
A weld parameter window is the range of output, time, dwell and force within which a seam passes both peel and immersion. Establishing it is the first job on any new shell, and it is done by welding at several settings, peeling the samples, immersing them and plotting where the passes sit. The window is then written down, and the window is what production runs to rather than a single setting.
Drift happens for four reasons and all of them are slow. Electrode faces wear and change thermal behaviour. Generators and heaters age. Ambient humidity changes the moisture content of the fabric, which changes how it responds to a dielectric field. And an operator who finds the cycle slightly slow will reduce the dwell, because the line is measured on output. Each shift is small; over a long run they compound.
The control is sampling through the run rather than at the start of it. Peel samples and immersion checks taken at the beginning, the middle and the end of a run catch drift while there is still time to correct it, and the record shows whether a lot was controlled or merely passed. Our process documentation under manufacturing sets out the interval, and the methods are listed under water ingress test methods.
Peel Strength Versus Hydrostatic Head at the Seam
Peel strength and water resistance are two different properties of the same seam and a seam can be excellent at one and poor at the other. Peel strength measures the force needed to separate the joined plies, and it predicts whether the seam survives being pulled, packed and dragged. Water resistance measures whether the same seam passes water under a head or during immersion, and it depends on continuity rather than on strength.
The interaction is not linear. Increasing energy beyond the optimum raises peel strength up to a point and then reduces it, because the coating is being degraded rather than fused. Meanwhile water resistance peaks in the middle of the window and falls off at both ends: too little energy leaves an unbonded channel, too much thins the coating until the seam no longer has a barrier. The strongest seam is not the most waterproof seam.
This is why a specification needs two numbers with two methods. Peel is measured on coated fabric to ASTM D751, and coated fabric waterproofness to ASTM D3393, while the shell itself is qualified to ISO 811 or AATCC 127 for hydrostatic head. A supplier quoting only a hydrostatic figure has told you about the fabric and not about the seam, which is where your bag will actually fail.
Seam Failure Modes Found in Warranty Returns
Field returns cluster into five seam failure modes, and each has a distinct appearance. A cold weld shows as a seam that looks correct and separates cleanly at the interface with no material transfer, meaning the coating never fully melted. A burnt weld shows discolouration, bubbling or a thin glazed line, meaning too much energy. Both are parameter failures rather than design failures.
A stepped ply failure shows as a channel at a multi-ply corner where the electrode could not press evenly, and it is a tooling and design issue that no parameter change will fix. A contamination failure is intermittent, appears at random positions along a seam and is usually traceable to handling at the weld station. A flex fatigue failure appears after repeated folding in the same place, most often at a roll-top mouth, and it is a material and geometry issue.
Distinguishing them matters because the fixes are different and the cost of the wrong fix is a second failed season. Cold welds are fixed in the parameter window, burnt welds likewise, stepped plies by redesigning the corner or re-machining the electrode, contamination by station discipline, and flex fatigue by changing the shell or the fold radius. A supplier who diagnoses the mode before quoting the fix is worth keeping.
Seam Leak Detection at the Bench and on the Line
Three detection methods are used on welded seams and they find different things. Visual inspection under good light finds gross defects: incomplete welds, burns, misalignment. It is fast, it is cheap and it finds almost nothing that matters at the sub-millimetre scale, which is where a pinhole lives. Immersion testing finds leaks but only where the leak is large enough to admit water within the test duration.
Air pressure testing is the sensitive method. The bag or the seam channel is inflated to a low pressure and the decay rate is measured over a set period. A seam that passes immersion comfortably can fail a pressure decay test, because air escapes through an orifice that water will not enter against surface tension. Where a buyer is shipping a product that must stay dry rather than merely resist rain, pressure decay is the appropriate gate.
The practical arrangement is to run all three at different points: visual on every unit, pressure decay on a sample from the beginning, middle and end of the run, and immersion on finished units as a confirmation. That layering is what makes a defect rate meaningful, and it is the structure behind the inspection sampling described under quality and inspection.
Low-Temperature Seam Flex and Freeze Cycling
A welded seam is a re-solidified region of coating, and it is stiffer than the fabric around it. At low temperature the whole shell stiffens, but the seam stiffens disproportionately, so the flex load concentrates at the boundary between the seam and the parent material. Repeated folding at that boundary in cold conditions is one of the most reliable ways to initiate a seam crack, and it is entirely absent from a room-temperature test programme.
The test is straightforward and worth specifying. Condition the finished bag at a low temperature for a defined period, flex the seam through a defined angle for a defined number of cycles, then return it to ambient and re-run the immersion or pressure decay test. A seam that passes at ambient and fails after cold flexing will fail in a ski season, a winter commute or a mountain trip, all of which are predictable use cases.
The design mitigation is a radius. Where a seam has to fold in service, the fold should occur in parent fabric with a generous radius rather than at the seam boundary, and the seam should be kept away from the fold line by a margin. That one drawing decision prevents more cold-weather seam failures than any change to the weld parameters, and it costs nothing at the tooling stage.
The material side of the same problem is coating selection. Two shells with identical hydrostatic figures at ambient temperature can behave very differently after cold flexing, because the glass transition of the coating governs where it stiffens. A programme intended for a winter market should therefore qualify the shell on its cold-flex behaviour rather than on its room-temperature rating, and should name the conditioning temperature and cycle count on the specification.
Seam Spec Wording for a Welded Bag Order
The seam paragraph of a specification should name five things: the method, the seam width in millimetres, the peel acceptance value with its test method, the leak test with its acceptance criterion, and the sampling plan. Anything less leaves the most failure-prone part of the bag governed by goodwill rather than by an enforceable number. Method and width alone, which is what most specifications contain, describe how the seam was made and not whether it works.
Add two clauses that cost nothing and resolve most disputes. The first requires a retained seam sample from the approved run, signed off, stored flat and dated. The second requires the recorded parameter window to be supplied with the golden sample, because a sample without its parameters cannot be reproduced and a dispute cannot be settled against it.
Finally, state the acceptance standard for the shipment. Inspection to AQL 2.5 under ISO 2859-1 with critical, major and minor classifications agreed in advance means a seam defect is either critical or it is not, decided before the inspection rather than argued during it. That single sentence is the difference between an inspection report that resolves a dispute and one that starts one.
Seam Cycle Time and Cost on a 500-Piece Run
Seam method is one of the larger drivers of unit cost on a welded bag, because it sets the labour content and the capital utilisation of the line. An RF press produces a complete seam in one cycle and the operator loads and unloads; a hot air line runs continuously and the operator manages speed and pressure; a taped seam needs two operations, stitching followed by taping, each with its own handling.
At 500 pieces per style per colour, setup and trial time is a meaningful share of the total, which is why the method chosen for sampling should be the method intended for production. A bag sampled on hot air and produced on RF, or the reverse, will not come out the same, and the difference will be discovered at goods-in rather than at approval. Methods are not interchangeable mid-programme.
The cost question buyers should therefore ask is not which method is cheapest per seam but which method the geometry suits, because a method fighting the geometry produces scrap, rework and a slower line than a nominally more expensive method working with it. We quote the method alongside the seam spec so the two can be evaluated together, and full programme detail sits under product programmes.
Frequently Asked Questions
Q1: Why do waterproof bags leak at the seam rather than through the fabric?
A: The shell fabric carries a coating or laminate rated at 10,000 mm on lightweight styles and 20,000 mm and above on load-bearing ones, and it holds that across its whole area. The seam is where two coated faces have been melted and re-solidified, so the barrier there is only as good as that operation. Most field failures are joins, not panels.
Q2: What are the main seam sealing methods for waterproof bags?
A: Six are in regular use: radio frequency welding, which heats the coating by dielectric loss; hot air and hot wedge welding, which heat by convection and contact; ultrasonic welding for hardware tabs and small features; tape applied over a stitched seam; and a stitch-and-tape hybrid where a welded seam meets a load-bearing assembly.
Q3: When is hot air welding better than RF welding?
A: Hot air is better where the TPU grade does not respond well to a dielectric field, and where the shell carries a surface finish that interferes with RF. It heats by convection, so it is far less sensitive to coating chemistry. The trade-off is more variables for the operator to hold steady and a slower line speed than a single RF press cycle.
Q4: Is a stronger seam also a more waterproof seam?
A: No, and this is one of the most important distinctions in the category. Peel strength and water resistance peak at different points in the parameter window. Too little energy leaves an unbonded channel that leaks; too much degrades or thins the coating until the barrier is gone. The strongest weld is rarely the most waterproof one.
Q5: Which tests should a welded seam specification name?
A: Name peel strength on coated fabric to ASTM D751, coated fabric waterproofness to ASTM D3393, hydrostatic head on the shell to ISO 811 or AATCC 127, and a leak test with its acceptance criterion. Add the sampling plan. A hydrostatic figure alone tells you about the fabric and says nothing about the seam.
Q6: How are seam leaks detected in production?
A: Three methods, layered. Visual inspection on every unit finds gross defects but misses pinholes. Immersion finds leaks large enough to admit water. Air pressure decay is the sensitive method, because air escapes through an orifice that water will not enter against surface tension, so it catches seams that pass immersion.
Q7: What causes a seam to fail after a season of use?
A: Five modes appear repeatedly: a cold weld that separates cleanly with no material transfer, a burnt weld showing discolouration or bubbling, a channel at a multi-ply corner, intermittent contamination at the weld station, and flex fatigue after repeated folding at a roll-top mouth. Each has a different fix.
Q8: Do welded seams work in cold weather?
A: They work, but they are stiffer than the fabric around them and they stiffen disproportionately as temperature falls, so flex load concentrates at the seam boundary. Condition a bag cold, flex the seam through a set angle for a set number of cycles, then re-test for leaks. Design the fold to occur in parent fabric away from the seam.
Q9: Can any coated fabric be welded or taped?
A: No. Welding requires a consistent coating that melts predictably, and taping requires a coating the adhesive can grip. Some low-cost coated fabrics have coatings inconsistent enough to fail both routes, which is why a shell should be trial-welded and trial-taped before it is ever committed to a style on the strength of a data sheet.
Q10: What should the seam paragraph of a spec sheet say?
A: Name five things: the sealing method, the seam width in millimetres, the peel acceptance value with its test method, the leak test with its acceptance criterion, and the sampling plan. Add a requirement for a retained signed seam sample and for the recorded parameter window to be supplied with the golden sample.
Q11: How does seam method affect unit cost at 500 pieces?
A: Method sets labour content and capital utilisation. An RF press completes a seam in one cycle, a hot air line runs continuously and is operator dependent, and a taped seam needs stitching and taping as two operations. At 500 pieces the setup and trial share is significant, so the method used for sampling must be the method used for production.
Q12: What sampling level applies to seam inspection?
A: Inspection runs to AQL 2.5 under ISO 2859-1 for both incoming material and finished goods, with critical, major and minor classifications agreed before the inspection. Seam defects are sampled from the beginning, middle and end of the run rather than only at setup, so that parameter drift during the run is visible in the record.
Q13: How long does it take to qualify a seam method for a new style?
A: Trial welding a candidate shell at three points across the parameter window, peeling and immersing the samples and recording the window is part of standard sampling, which runs 6 to 10 working days from frozen drawings, or 12 to 15 working days where the programme is complex. Bulk production then takes 35 to 50 days from sample approval.
People Also Ask
- What is the strongest seam for a waterproof bag?
- Is RF welding better than seam tape?
- How do you test if a welded seam leaks?
- Why does my dry bag seam split in cold weather?
- What is seam peel strength?
- Can TPU be welded with hot air?